News & Blogs

Why Choose Pp Non Woven Fabric for Global Sourcing?

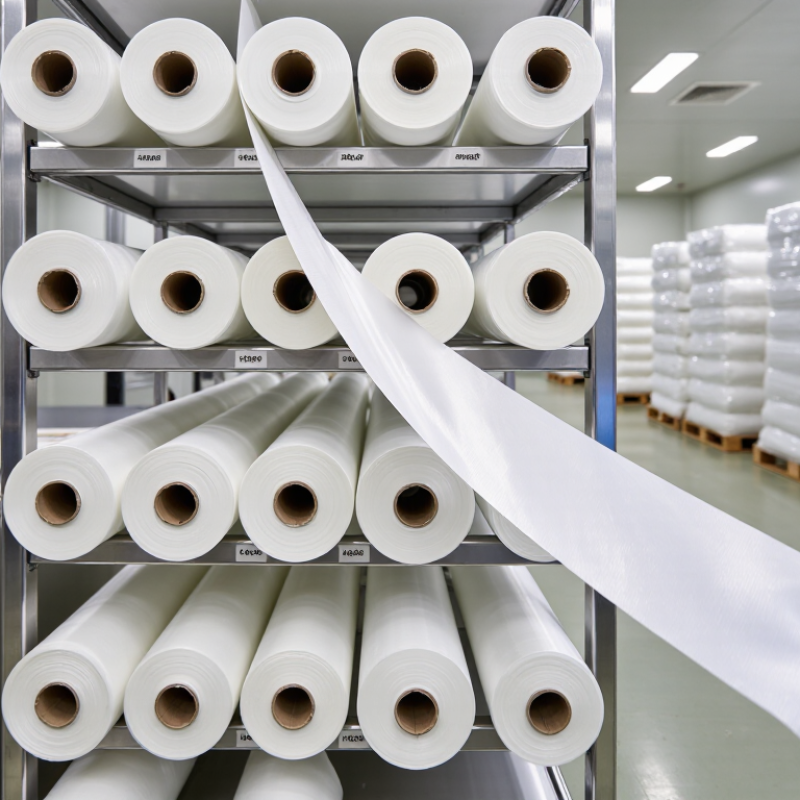
Choosing Pp Non Woven Fabric for global sourcing involves more than comparing unit prices. Buyers must examine performance, supplier capability, and delivery reliability. This material is widely used in shopping bags, medical packaging, agriculture covers, and hygiene products. Its lightweight structure can reduce shipping volume and handling costs. That matters when containers travel across long supply routes.

Experienced sourcing teams usually request samples before approving production. They check thickness, tensile strength, softness, color consistency, and sealing performance. A sample may feel suitable by hand, yet fail during stitching or heat sealing. Small differences can affect an entire shipment. Real factory audits also reveal practical details, including clean storage areas, calibrated testing equipment, and stable production records.

Pp Non Woven Fabric is not a universal answer. It can lose suitability when buyers ignore humidity, temperature, load requirements, or end-use conditions. Some assumptions fail. Suppliers should provide clear technical data, batch information, and transparent quality procedures. Buyers should also confirm packaging standards, documented certifications, and import requirements for the destination market. Requirements differ across countries and product categories, so independent verification remains important.

A dependable supplier communicates limits, not only advantages. That honesty supports better decisions. Global sourcing works best when price, quality, traceability, and service are evaluated together. The right material is not simply the cheapest roll. It is the option that performs consistently from factory floor to final application.

Why Choose Pp Non Woven Fabric for Global Sourcing?

PP Nonwoven Basics: 0.90–0.91 g/cm³ Density and 160–170°C Melt Range

Why Choose PP Nonwoven Fabric for Global Sourcing?

PP nonwoven fabric starts with a useful physical advantage: polypropylene density is typically 0.90–0.91 g/cm³. ASTM D792 provides the common density-testing method. This low density helps produce lightweight rolls, bags, medical covers, and filtration layers without feeling flimsy. In a warehouse, the difference is practical. More meters can fit into each carton, although final savings depend on basis weight and packing design.

The usual PP melt range is about 160–170°C, based on thermal testing principles described in ASTM D3418. This range supports stable extrusion and spunbond processing when temperature control is properly calibrated. It is not a universal setting. Grade, additive content, line speed, and moisture can shift actual behavior. Small temperature errors may create weak bonding or uneven webs. That detail is easy to overlook.

PlasticsEurope’s Plastics—The Facts 2023 reported global plastics production of 400.3 million tonnes in 2022, showing the scale of polymer sourcing and conversion. For buyers, scale does not replace verification. Request density, melt-flow, basis-weight, and tensile test results from each shipment. The 2024 Global Nonwovens Industry Report also highlights continued demand across hygiene, healthcare, construction, and filtration applications. PP fits many of these uses, but “fits” is not “proven.” Trial production remains necessary, especially when switching suppliers or equipment.

Performance Testing: GSM, Tensile Strength, and Elongation Under ISO 9073

Why Choose PP Non Woven Fabric for Global Sourcing?

Performance testing gives buyers measurable evidence before large-scale sourcing. Under ISO 9073, GSM testing measures fabric mass per unit area. It affects coverage, softness, stiffness, and production yield. A calibrated balance and representative samples are essential. Small sampling errors can distort the result.

Tensile strength and elongation are equally important. ISO 9073-3 testing commonly examines machine direction and cross direction separately. The machine direction may resist pulling better, while the cross direction may stretch more. Test reports should show peak force, elongation at break, specimen size, and test conditions. Conditioning matters. Humidity and temperature can change PP fabric behavior.

In practical sourcing work, I compare several rolls, not just one laboratory sample. A fabric with higher GSM is not automatically stronger. That assumption can waste material and increase shipping costs. I also check whether elongation suits the final use, such as wrapping, filtration, or protective layers. Too little elongation may cause tearing during handling. Too much may reduce dimensional stability. Results sometimes disagree between batches. That is not unusual, but it deserves investigation. Consistent testing, clear records, and calibrated equipment make supplier comparisons more reliable. Even then, test data cannot replace a small production trial.

Filtration Selection: BFE ≥95% Under EN 14683 for Medical Applications

Polypropylene nonwoven fabric is widely considered for global sourcing because it is lightweight, scalable, and suitable for layered medical filtration structures. In medical applications, bacterial filtration efficiency remains a critical checkpoint. Under EN 14683, a BFE result of at least 95% supports Type I mask performance, while higher classifications require stricter results.

The filtration layer usually relies on fine meltblown fibers positioned between protective spunbond layers. This structure helps capture bacterial particles while maintaining practical breathability. Ask suppliers for complete EN 14683 test reports, not only a number printed on a specification sheet. The report should identify the laboratory, test method, sample details, and production batch.

Check the material closely. Consistent fiber formation matters. Uneven areas can create weak filtration zones, even when an average result looks acceptable. Pressure differential should also be reviewed, because high filtration with uncomfortable airflow may reduce real-world use. Storage conditions deserve attention too. Moisture, dust, and poor packaging can affect surface cleanliness and handling.

A certificate is not enough.

For reliable sourcing, compare samples from multiple batches and confirm traceability from resin to finished roll. Medical mask performance depends on the complete product design, including sealing, assembly, and quality control. The fabric alone does not prove final compliance. Some procurement decisions still rely too heavily on price. That can be a costly mistake. Independent verification remains sensible when the application involves patient care or clinical environments.

Why Choose PP Non Woven Fabric for Global Sourcing? - Filtration Selection: BFE ≥95% Under EN 14683 for Medical Applications

Technical sourcing reference for polypropylene (PP) spunbond, meltblown and composite nonwoven materials used in medical face-mask applications.
Sourcing Dimension Recommended Specification Relevant Benchmark or Standard Why PP Nonwoven Is Suitable Verification Method
Bacterial Filtration Efficiency (BFE) ≥95% for Type I medical face masks EN 14683:2019+AC:2019, Type I classification A PP meltblown filtration layer can provide high particle capture while maintaining a lightweight structure when properly engineered. Request an accredited laboratory test report using the EN 14683 BFE method. Confirm the tested finished mask construction rather than relying only on raw-material claims.
Higher Filtration Option ≥98% for Type II and Type IIR masks EN 14683:2019+AC:2019, Type II and Type IIR classifications Layered PP structures can be adjusted through meltblown basis weight, fiber diameter, electrostatic charging and laminate design. Verify BFE results together with differential-pressure and, where applicable, splash-resistance results for the complete product.
Differential Pressure ≤40 Pa/cm² for Type I and Type II; ≤60 Pa/cm² for Type IIR EN 14683:2019+AC:2019 PP nonwoven is lightweight and air-permeable, supporting a balance between filtration performance and wearing comfort. Test the finished mask under the EN 14683 differential-pressure procedure. Do not evaluate breathability from fabric weight alone.
Splash Resistance ≥16.0 kPa for Type IIR applications EN 14683:2019+AC:2019, Type IIR A hydrophobic PP outer layer can help resist liquid penetration when the total mask construction is appropriately designed. Use the EN 14683 synthetic-blood splash-resistance test on the finished mask. Hydrophobicity by itself does not prove Type IIR compliance.
Microbial Cleanliness ≤30 colony-forming units per gram (CFU/g) EN 14683:2019+AC:2019 PP is a synthetic polymer and does not provide a nutrient source for microbial growth; cleanliness still depends on manufacturing and packaging controls. Obtain a microbial-cleanliness test report and review production-area hygiene, handling, storage and packaging procedures.
Typical Layer Configuration Spunbond / meltblown / spunbond (SMS) or an equivalent multi-layer PP construction Common medical nonwoven construction; final performance must be tested against the applicable standard Spunbond layers provide handling strength and protection, while the meltblown layer performs the primary filtration function. Request a layer diagram, material declaration, basis-weight breakdown and representative production samples.
Polymer Composition Predominantly polypropylene; confirm additives and colorants Material specification established by the purchaser and supplier PP has a low density of approximately 0.90–0.91 g/cm³ and is commonly processed into lightweight nonwoven webs. Review the technical data sheet, safety data sheet and, when required, polymer identification or composition testing.
Thermal Processing Consideration Typical PP melting range: approximately 160–170°C, grade-dependent Polymer-grade property; confirm the specific resin data sheet The material can be converted into fine fibers by melt processing without solvent use, supporting scalable nonwoven production. Confirm the exact resin grade, melt-flow information, processing window and compatibility with converting equipment.
Moisture and Water Behavior Low moisture absorption; hydrophobic surface behavior General PP material property; not a substitute for EN 14683 testing Low water uptake can support stable handling and protect the intended dry-web filtration structure during normal storage. Check moisture-related specifications, packaging requirements and finished-product performance after conditioning.
Basis Weight Selection Use a validated construction rather than a universal target; common medical-mask layers may range from lightweight to medium-weight nonwovens Supplier- and design-dependent; EN 14683 specifies performance, not one fixed fabric basis weight Filtration depends on multiple variables, including fiber diameter, web uniformity, electrostatic charge, thickness and airflow resistance. Compare basis weight, thickness, air permeability, BFE and differential pressure using samples from the intended production route.
Supply-Chain Consistency Lot traceability, controlled specifications and retained samples Quality-system requirement established by the sourcing program PP nonwoven production can be scaled across different converting locations when resin, process settings and test criteria are controlled. Audit batch records, certificate-of-analysis procedures, change-control processes and incoming inspection plans.
Packaging and Storage Clean, sealed packaging; protection from dust, moisture, heat and prolonged direct sunlight Follow supplier instructions and applicable medical-device quality requirements Appropriate packaging helps preserve cleanliness, web integrity and the performance of electrostatically charged filtration media. Define storage temperature, humidity, shelf-life evidence, packaging integrity checks and transport conditions.
Compliance Documentation Current test reports, technical data sheet, declaration of materials and lot-level records EN 14683 for medical face-mask performance; other regulatory requirements may apply by destination market A standardized PP material platform can simplify documentation when each finished configuration is tested and controlled. Verify report scope, sample identity, test date, laboratory competence, production-lot connection and applicable market requirements.
Important: EN 14683 classifies the finished medical face mask, not PP fabric solely by itself. BFE ≥95% corresponds to the Type I threshold, while Type II and Type IIR require BFE ≥98%. Actual compliance depends on the complete mask design, manufacturing controls, labeling and applicable regulatory requirements in the destination market.

Global Compliance: REACH, RoHS, and ISO 9001 Supplier Controls

Why Choose PP Non-Woven Fabric for Global Sourcing?

Global Compliance: REACH, RoHS, and ISO 9001 Supplier Controls

PP non-woven fabric supports global sourcing through low weight, stable processing, and flexible design. Yet compliance needs more than a material declaration. REACH evaluates chemical risks across the supply chain. RoHS restricts ten hazardous substances in applicable electrical and electronic products. Requirements can change with the product’s final use.

The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates worldwide. This figure shows the scale of certified quality management. It does not guarantee every shipment is consistent. A reliable supplier should connect ISO 9001 controls with batch records, incoming inspection, process checks, and corrective actions. For REACH, request current SVHC screening and supporting laboratory evidence. For RoHS, confirm testing methods, sample identity, and report dates. Paperwork alone is not enough. In practical sourcing, mismatched batch numbers remain an overlooked weakness.

Tips: Ask for a compliance matrix before sampling. Check polymer grade, additives, colorants, and packaging separately. Require traceability from resin lot to finished roll. Independent testing can confirm supplier declarations, especially for high-volume orders. Keep the documents with purchase records. This sounds simple, but teams often miss it during urgent launches. A second review may feel slow. It can prevent costly rework, rejected cargo, and unclear accountability.

Sourcing Economics: GSM, MOQ, Lead Time, and Landed Cost at Scale

Why Choose PP Non Woven Fabric for Global Sourcing?

Sourcing Economics: GSM, MOQ, Lead Time, and Landed Cost at Scale

PP non woven fabric can support global sourcing when buyers measure more than the unit price. GSM directly affects strength, coverage, material use, and shipping weight. A 25 GSM roll may reduce freight, but it can fail when handling demands higher tear resistance. A 60 GSM option costs more, yet it may reduce waste during production. Small changes matter.

MOQ also shapes the real purchasing decision. A low MOQ helps buyers test colors, widths, and end-use performance before committing heavily. Larger orders may unlock better conversion rates, but they can tie up cash and storage space. I have seen buyers chase the lowest quote, then pay more for unused inventory. That gap hurts. Request a clear price ladder by GSM, quantity, and packaging method.

Lead time needs practical checking, not optimistic promises. Ask about raw material availability, production capacity, inspection timing, and port schedules. A delayed shipment can disrupt cutting plans and customer deliveries. Calculate landed cost with fabric price, packaging, inland transport, freight, insurance, duties, inspection, and possible waste. Supplier records should support these figures. Sample testing remains essential. Fabric can look consistent while changing slightly between batches. That risk deserves a cost allowance. A careful sourcing plan compares performance per delivered kilogram, not price per kilogram alone.